We provide high-performance industrial lubricants, pumps, crushers, grinding equipment, and process solutions for mining, cement, energy, steel, plastics, and manufacturing industries.
Loading
We provide high-performance industrial lubricants, pumps, crushers, grinding equipment, and process solutions for mining, cement, energy, steel, plastics, and manufacturing industries.
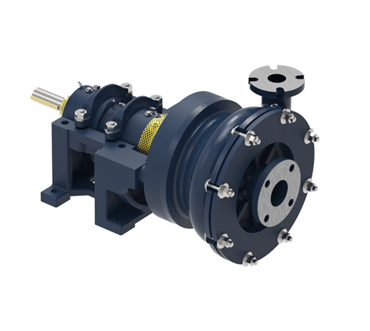
Air locking can reduce pump efficiency and availability. KREBS hMAX, slurryMAX, slurryMAX-XD, vMAX and vMAX-R pumps are designed to handle high air-entrained slurries with reliable and efficient performance.
The hMAX horizontal pump features a recessed impeller for high-froth applications, allowing entrained air to pass freely without affecting flow or head. Its concentric casing reduces radial loads and extends wear life.
The slurryMAX split-case mining slurry pump improves wear life and efficiency for abrasive mining and aggregate applications, delivering even, predictable wear with interchangeable material options.
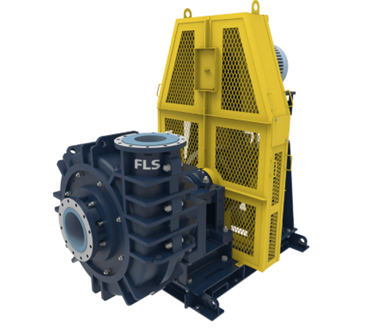
The slurryMAX-XD horizontal pump combines a heavy-duty impeller with thick, steel-reinforced elastomer linings to extend wear life in aggressive applications such as cyclone feed, regrind, and tailings.
The vMAX pump features optimized hydraulics for handling large solids and viscous fluids. Bottom-only suction prevents clogging, making it ideal for sump clean-up duties with extended wear life and dry-run capability.
The vMAX-R rubber-lined pump is designed for corrosive slurries with finer solids, offering adaptability to acid and temperature variations while ensuring long wear life.
KREBS heavy-duty pumps feature proprietary wear ring technology that reduces power consumption and extends wear life while handling abrasive slurries in demanding mineral processing applications.
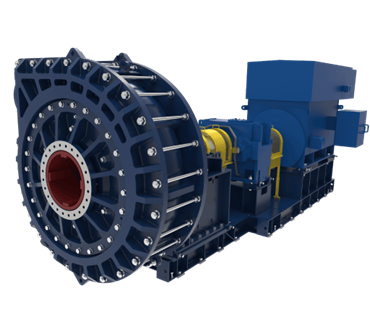
Designed for pumping large, abrasive solids, the gravelMAX pump prevents in-pump grinding with increased impeller clearance and ensures smooth solids discharge with enhanced durability.
The millMAX heavy-duty pump features a suction-side sealing system that improves mill throughput while delivering cost-effective slurry pumping and extended wear life.
Built for aggressive duties like cyclone feed and tailings, the slurryMAX-XD pump provides predictable wear, material flexibility, and superior durability.
The UMD Ultimate Mill Discharge pump offers optimized hydraulic performance, even wear, up to 10% lower power consumption, and flexible duty operation for abrasive mining conditions.
The UMD-R fully rubber-lined split-case pump is ideal for corrosive applications, delivering even wear, low cost per tonne pumped, and reliable performance.
High-pressure slurry applications demand the toughest pumps. KREBS millMAX™, slurryMAX™-HP, and UMD™ high-pressure pumps thrive under extreme forces, delivering long-lasting, efficient pumping performance.
Designed for high total dynamic head applications, ideal for filter press feed and high-head pumping systems. Concentric casing ensures even velocity and pressure distribution, delivering long wear life and reduced cost per tonne pumped.
Handles operating pressures above 500 psi (35 bar). Features robust casings, superior hydraulic efficiency, and durable wear linings for extended wear life and reduced operating costs.
Engineered for high-pressure multi-stage duties with strong casing MOBIL and optimized wear protection. Delivers predictable performance and lower power consumption.
Designed for coarse tailings and hydro-transport duties. Provides even wear, lowest cost per tonne pumped, and 5–10% lower power for the same flow and head.
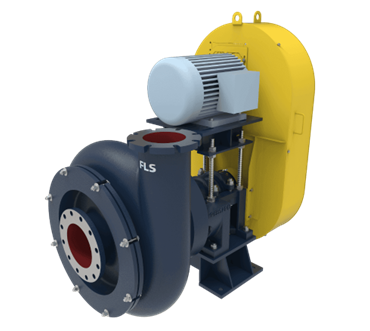
FLS KREBS® gravelMAX™ and UMD™ pumps feature large internal clearances to handle slurries with large, abrasive solids without grinding, delivering higher throughput and extended wear life.
Designed for pumping large, abrasive solids. Increased clearances prevent grinding and can deliver up to 100% longer wear life than conventional slurry pumps.
Optimized hydraulic design ensures maximum efficiency and even wear in demanding mill discharge applications, with up to 10% lower power consumption.
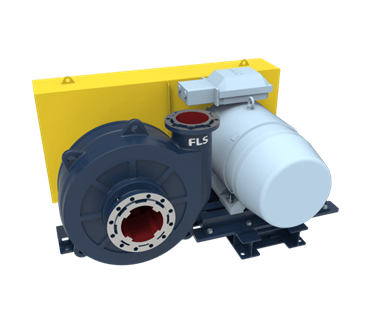
millMAX™-e, hMAX™, and slurryMAX™ pumps deliver high-efficiency, low-maintenance performance for mining and industrial applications.
Recessed impeller and large internal clearances minimize product degradation and air locking while handling large solids efficiently.
Compact design reduces power consumption and total pumping costs while maintaining high reliability and performance.
Horizontal centrifugal pump offering improved wear life, interchangeable materials, and no gland water requirements.
Designed for pumping large, abrasive solids. Increased clearances prevent grinding and can deliver up to 100% longer wear life than conventional slurry pumps.
Optimized hydraulic design ensures maximum efficiency and even wear in demanding mill discharge applications, with up to 10% lower power consumption.
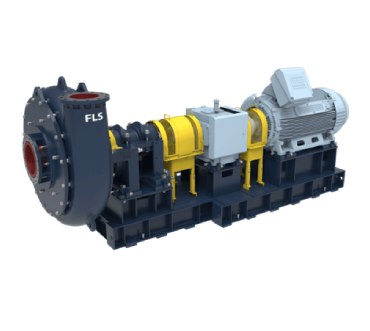
Built to handle abrasive grinding circuit slurries efficiently and reliably, maximizing wear life and lowering cost per tonne pumped.
Proprietary adjustable wear ring technology minimizes particle degradation, lowers power requirements by up to 10%, and improves mill throughput.
Heavy-duty impeller with steel-reinforced elastomer linings for aggressive applications such as hydrocyclone feed.
Optimized hydraulic efficiency with wide flow casing options and faster maintenance capability.
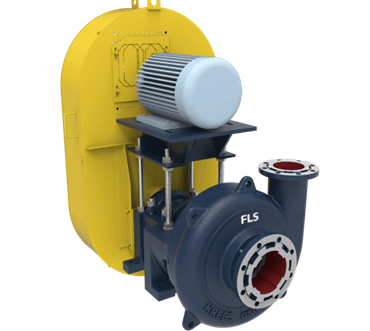
hMAX™ and vMAX™ recessed-impeller pumps handle challenging slurries with ease, preventing product degradation and air locking, and are ideal for froth, large-particle, high-viscosity, and shear-sensitive mining and mineral processing applications.
Handles tramp material and large solids while minimizing shearing and air locking for extended wear life.
Bottom-only suction design prevents clogging and simplifies operation for sump clean-up duties.
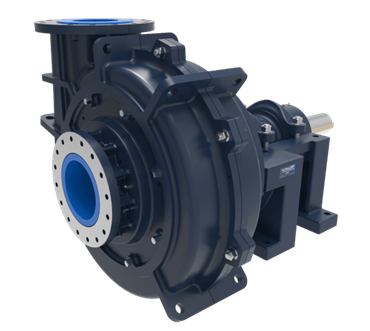
KREBS® split-case pumps are engineered for demanding applications, delivering durable, reliable, and efficient handling of abrasive mining slurries, extended uptime with versatile wear materials, and easier maintenance through their split-case design.
High-performance centrifugal seal eliminates gland water while delivering even wear and energy savings.
Designed for aggressive applications with predictable wear and superior durability.
Fully rubber-lined split-case pump providing even wear and reduced power consumption.
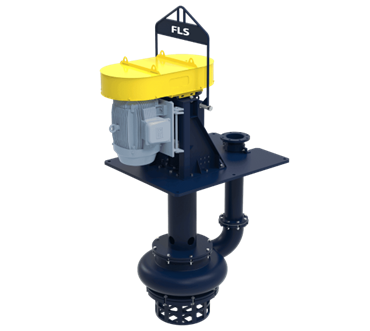
KREBS® vMAX™ vertical cantilever slurry pumps handle highly viscous fluids and large solids, preventing suction build-up, casing leakage, and excessive vibration for reliable operation.
Handles large solids and viscous fluids without clogging, ideal for clean-up sump duties.
Designed for corrosive slurries with fine solids and adaptable to various operating conditions.
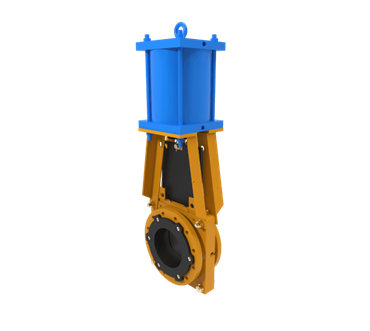
KREBS® heavy-duty knife gate, check, and vacuum breaker valves reduce CAPEX and maintenance costs
Full range of flanged, wafer, high-pressure knife gate, vacuum breaker, and check valves for mineral processing lines